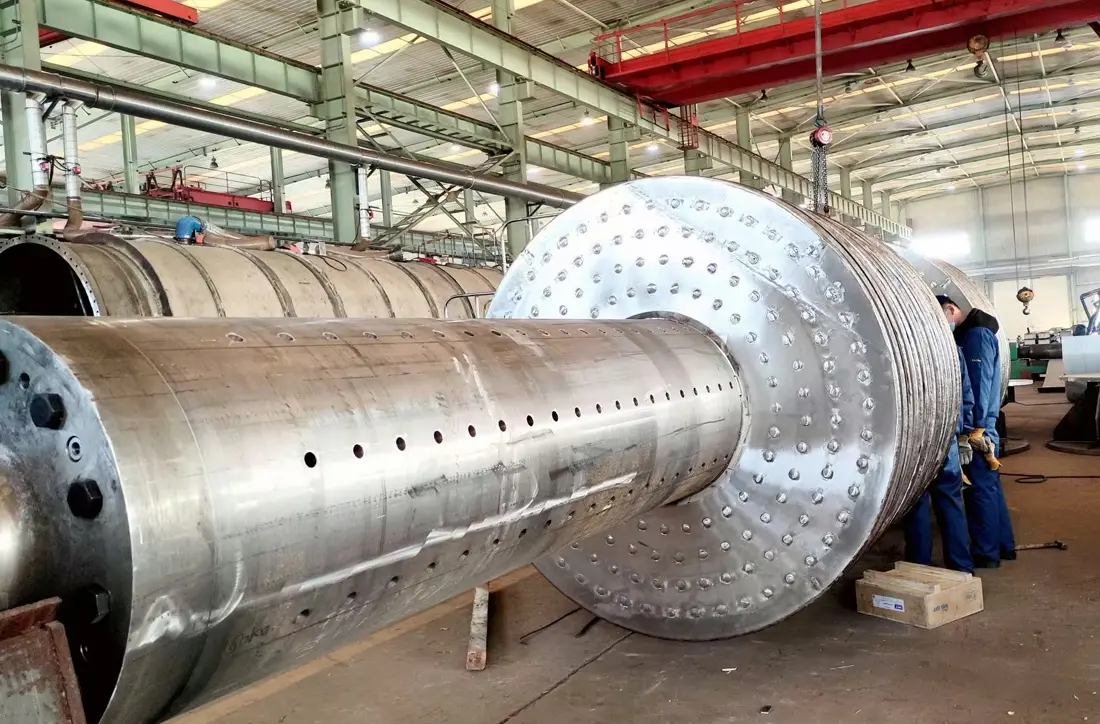
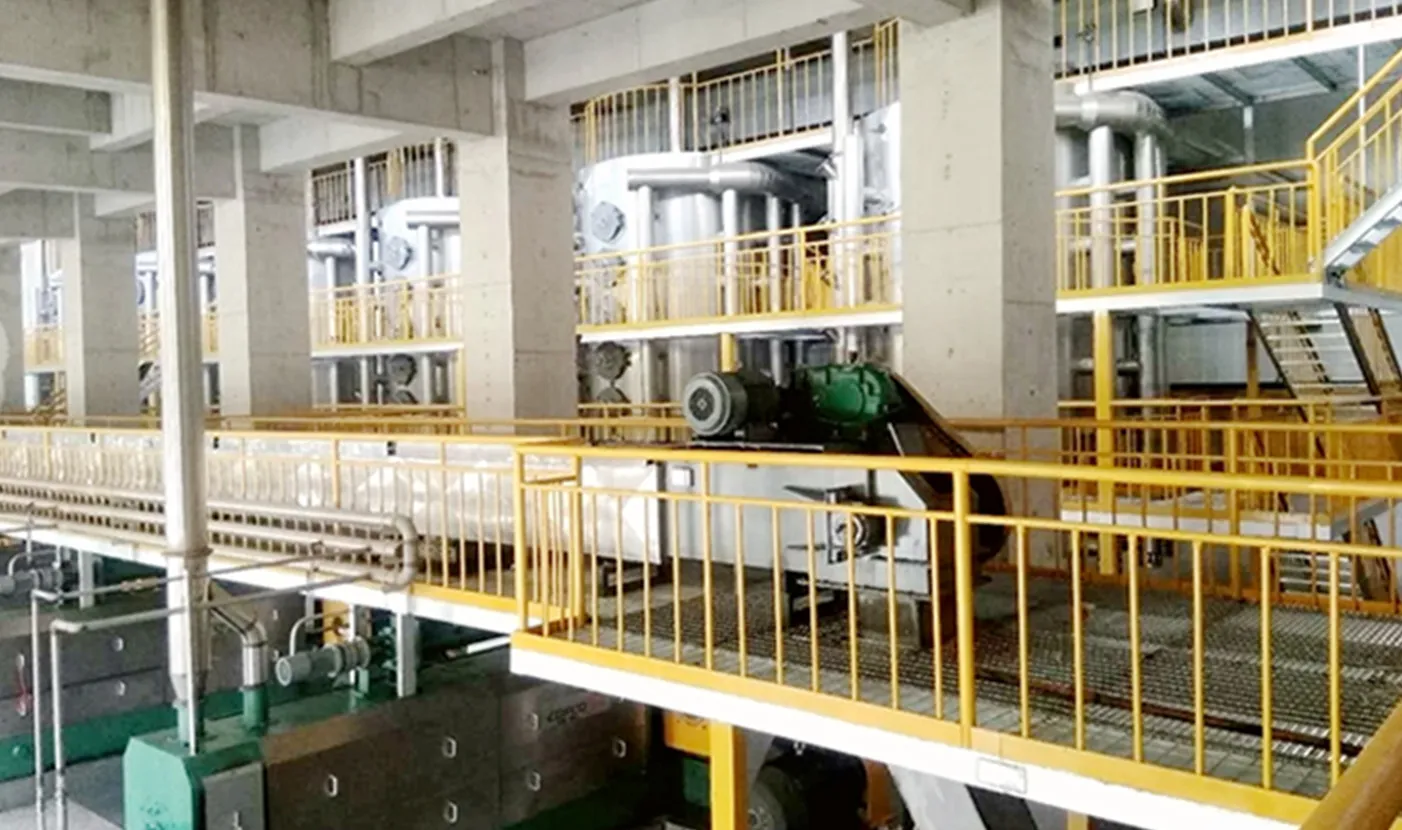
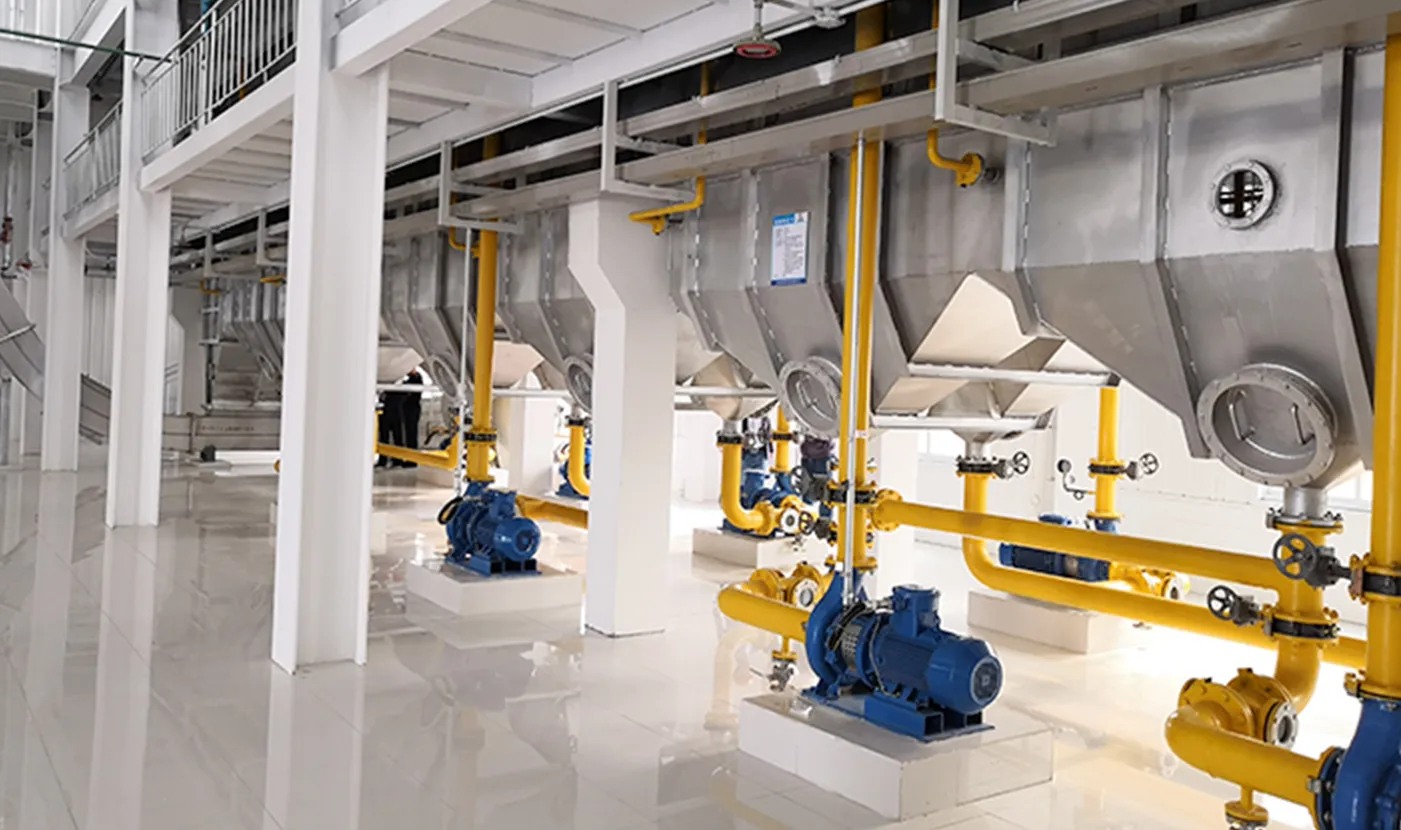
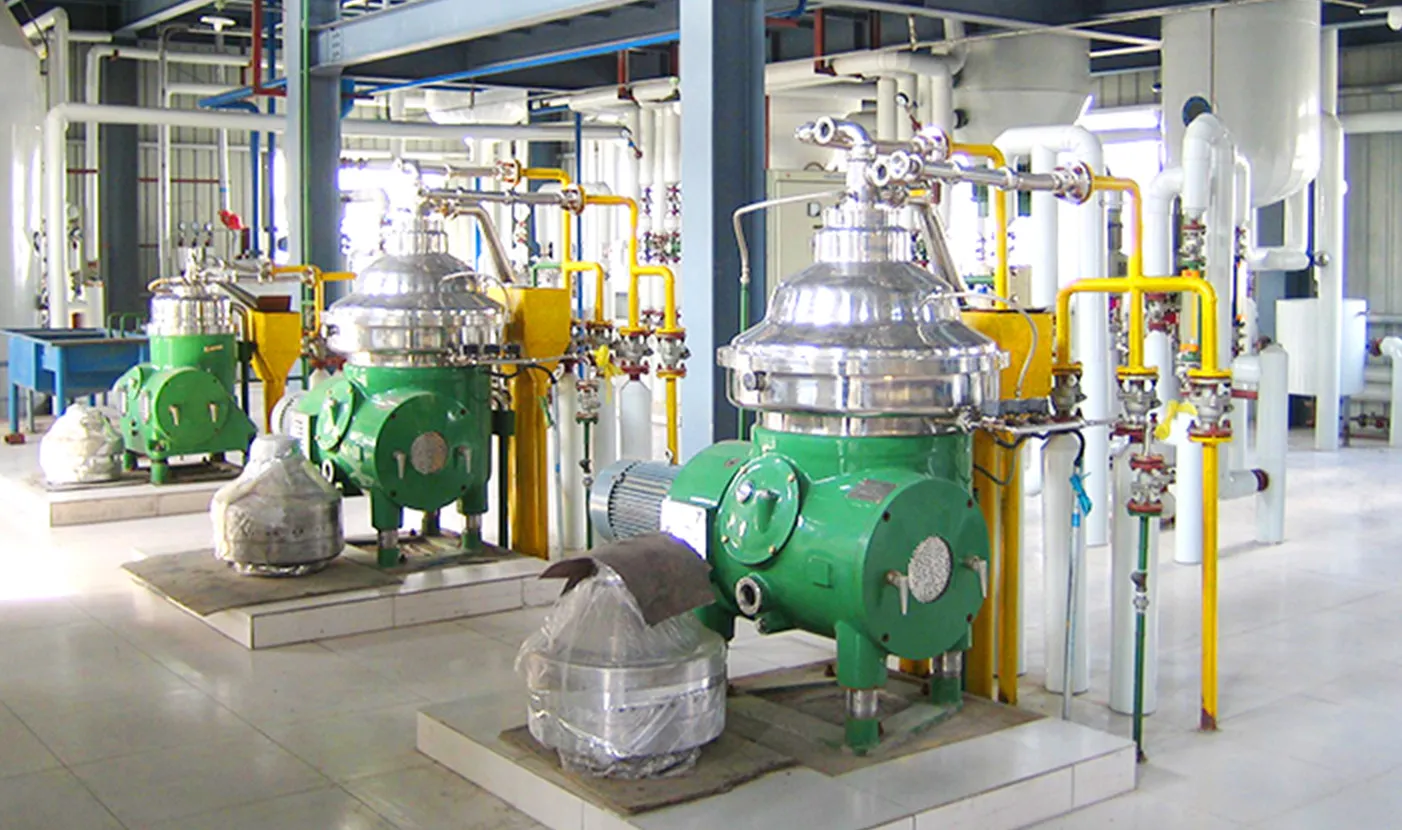
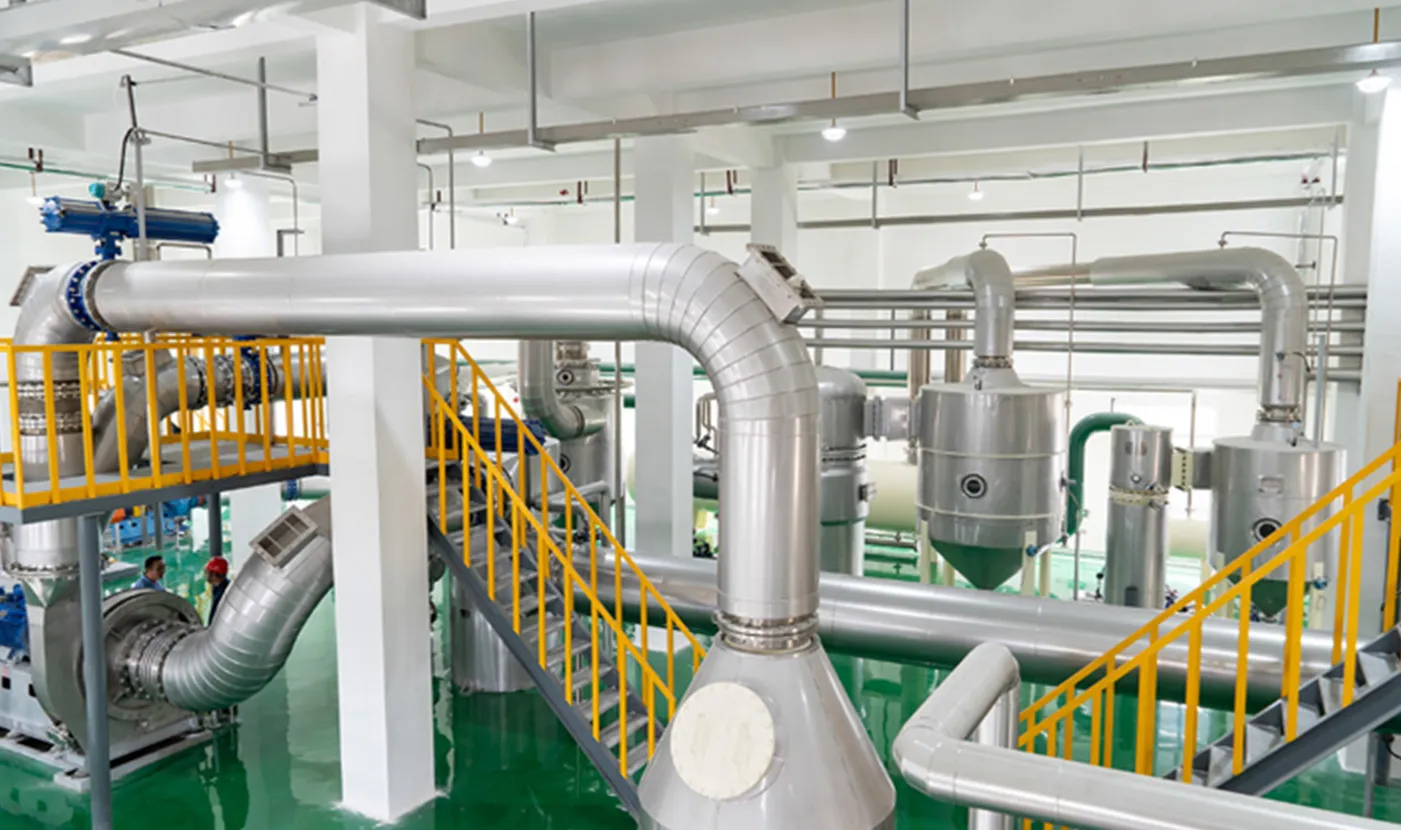
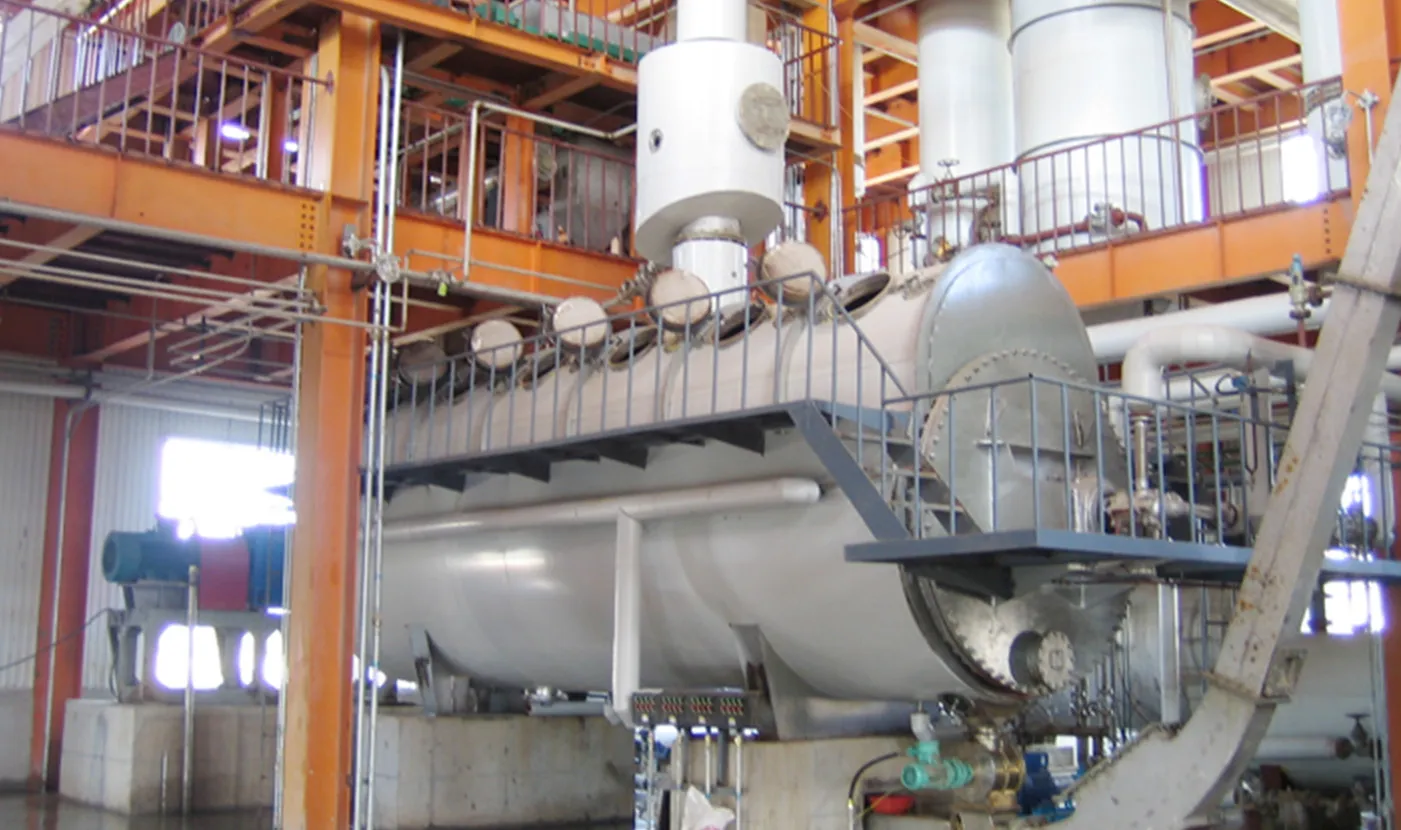
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Sunflower Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Rapeseed Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Peanut Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Cotton Seed Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Corn Germ Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Rice Bran Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Sesame Oil Production Line
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Soybean White Flake
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Soybean Protein Concentrate (SPC)
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Soybean Protein Isolate (SPI)
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Peanut Protein
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Cottonseed Protein
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Sunflower Protein
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
Other Vegetable Protein
Soybean meal has high requirements for fat content, powder fineness, color and NSI value because it is extensively used as a raw material for production of SPC, SPI, histone and wiredrawing protein. CHEMSTA provides various soybean intensive processing lines, one of which is suitable for production of low temperature soybean meal.
The extractor is the core equipment of an extraction workshop. Among all extractor types, the drag chain extractor features cutting-edge technology, strong material adaptability and superior performance.
Screw Oil Press
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Flap Cooler
Depending on the type of oilseed, different pretreatment, pressing, puffing, and solvent extraction processes are employed to produce high-quality meal and edible oils through a mechanized, continuous production line with a fully computerized, automated production process.
Expander
When preparing seeds for oil extraction, the seed needs to be heated and dried to the correct temperature and moisture.
Softening Cooker
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Aspirator
Depending on the type of oilseed, different pretreatment, pressing, puffing, and solvent extraction processes are employed to produce high-quality meal and edible oils through a mechanized, continuous production line with a fully computerized, automated production process.
Crushing Machine
When preparing seeds for oil extraction, the seed needs to be heated and dried to the correct temperature and moisture.
Flaker
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Oil solvent stripping tower
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Deodorization tower
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Horizontal desolventizer B
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
Evaporator
A screw press consists of a continuous, helical thread that revolves within a stationary, perforated cylinder.
In recent years, the demand for plant-based protein ingredients has grown rapidly across the global food industry. This shift is driven by changes in consumer eating habits, increased focus on health nutrition, and the expansion of functional food manufacturing. Among all plant protein ingredients, soybean protein isolate has become one of the most widely used due to its high protein concentration and versatile functionality.
According to multiple food science and nutrition research summaries, plant protein demand has been increasing year by year, with soy-based ingredients remaining a core contributor because of their complete amino acid profile and cost efficiency. If you are working in food manufacturing or considering entering the protein ingredient market, understanding soybean protein isolate is essential for product development and sourcing decisions.
What Is Soybean Protein Isolate?
Soy protein isolate is a highly purified protein extracted from soybeans. It typically contains at least 90% protein content, with most fats and carbohydrates removed during processing. This makes it one of the most concentrated plant-based protein sources available.
Unlike whole soy flour or less refined soy protein products, soybean protein isolate is designed for functional applications in food systems. It provides emulsification, water retention, and texture improvement properties, making it highly valuable in processed food manufacturing.
In simple terms, it is not just a nutritional ingredient but also a functional food component used to improve product structure and stability.
How Soybean Protein Isolate Is Made
The production of soy protein isolate involves a controlled industrial process designed to separate protein from other soybean components.
The process begins with defatted soybean meal, which is obtained after oil extraction. The protein is then isolated through alkaline extraction and acid precipitation methods, followed by purification and drying.
Spray drying is commonly used to convert the purified protein into a fine powder form, which is easier to store and transport.
The overall process is carefully controlled to maintain protein integrity and functional properties.
Soybean Protein Isolate Production Process Flow
The industrial production process can be summarized as follows:
Stage
Process Description
Purpose
Raw material preparation
Cleaning and defatting soybeans
Remove impurities and oil
Protein extraction
Alkaline solution treatment
Dissolve protein from solids
Separation
Filtration and centrifugation
Separate protein liquid
Precipitation
Acid adjustment
Isolate protein fraction
Washing & purification
Remove non-protein components
Improve purity
Drying
Spray drying system
Produce powder form
This structured process ensures consistency in protein quality and functional performance across batches.
Nutritional Value of Soybean Protein Isolate
Soy protein isolate is considered a complete plant protein, meaning it contains all essential amino acids required by the human body. Research in food nutrition indicates that its digestibility is high, making it suitable for both general nutrition and sports-related applications.
It is commonly used in protein supplementation because it provides a balanced amino acid profile while being low in fat and carbohydrates. Compared to animal protein sources, it offers a plant-based alternative that aligns with modern dietary preferences.
Soybean Protein Isolate vs Other Protein Sources
To better understand its positioning, it is useful to compare soybean protein isolate with other common protein types:
Soy protein isolate vs soy protein concentrate
Soy protein isolate contains a higher protein level (around 90% or more), while soy protein concentrate typically contains 65–70% protein with more carbohydrates remaining.
Soy protein isolate vs whey protein
Whey protein is animal-based and known for fast absorption, while soybean protein isolate is plant-based and suitable for vegan and lactose-free diets.
Plant protein vs animal protein
Plant proteins like soybean isolate are often preferred for sustainability, dietary restrictions, and lower allergen diversity, while animal proteins may offer different absorption speeds.
Applications of Soybean Protein Isolate
Soy protein isolate is widely used across multiple food industries due to its functional versatility.
It is commonly applied in:
Meat substitutes and plant-based protein foods
Protein bars and nutritional snacks
Dairy alternative beverages
Bakery and processed food products
Sports nutrition formulations
Its ability to improve texture, moisture retention, and protein enrichment makes it a key ingredient in modern food formulation.
Advantages of Soybean Protein Isolate
There are several reasons why manufacturers prefer soybean protein isolate in product development:
First, it offers high protein concentration, which helps improve nutritional labeling and product positioning.
Second, it has low fat and carbohydrate content, making it suitable for health-focused formulations.
Third, it provides functional properties such as emulsification and gel formation, which improve food texture.
Finally, it is cost-effective compared to many alternative protein sources, especially in large-scale production environments.
Soybean Protein Isolate Production Equipment
Producing soybean protein isolate requires a series of specialized equipment designed for extraction, separation, and drying.
Key equipment includes:
Extraction tanks for protein solubilization
Centrifugation and filtration systems for separation
pH adjustment units for protein precipitation
Spray drying systems for powder formation
Quality control instruments for protein testing
A well-designed production line ensures efficiency, consistency, and product safety, which are critical for commercial supply.
Quality Standards and Safety
Soybean protein isolate used in food applications must meet strict quality standards. These include protein purity levels, microbial safety limits, and moisture content control.
Food-grade certification and quality testing are essential before distribution. Additionally, since soy is a known allergen, proper labeling and regulatory compliance are required in all markets.
Market Trends and Industry Outlook
The plant protein industry continues to grow as more consumers shift toward plant-based diets. Industry analyses show steady expansion in demand for soy-based protein ingredients due to their affordability and functionality.
Soybean protein isolate is expected to remain a core ingredient in food manufacturing because it supports both nutritional enhancement and product formulation flexibility. Its role in alternative protein products is particularly significant as food innovation continues to evolve.
Conclusion
Soybean protein isolate plays an important role in modern food manufacturing due to its high protein content, functional properties, and versatility. From nutritional supplements to plant-based food systems, it provides a reliable and efficient protein source for a wide range of applications.
For manufacturers and buyers, understanding its production process, quality standards, and application potential is essential for making informed decisions in a competitive and fast-growing industry.